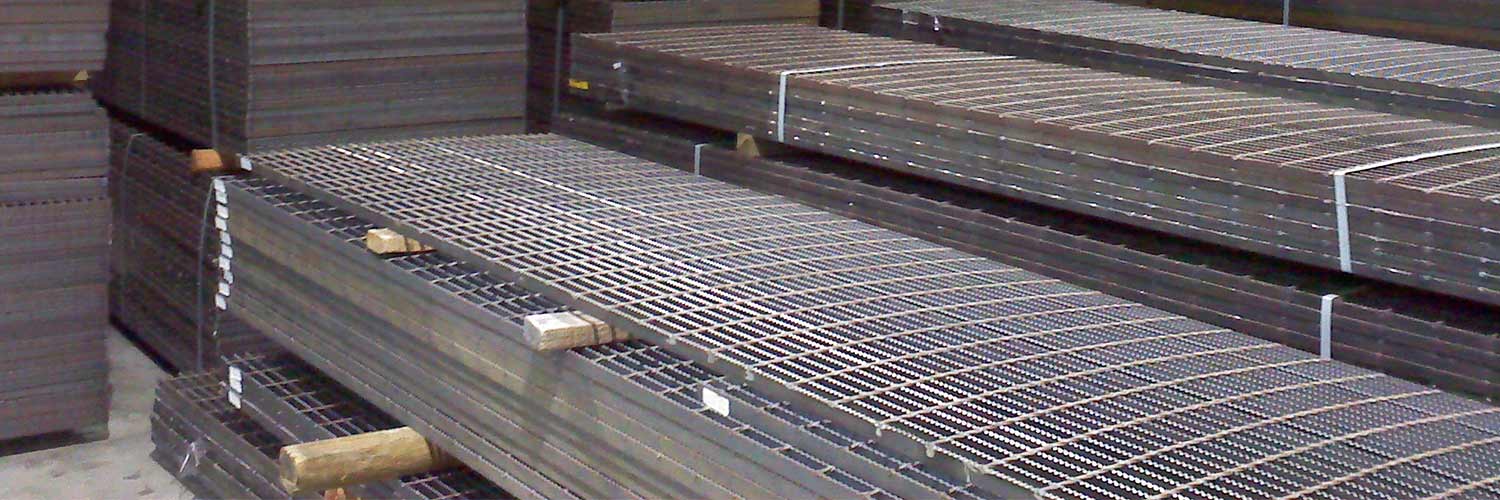
How do international EPC contractors, electrical grid engineers, and industrial procurement managers select, specify, and procure Galvanised Earthing Strips (GI Grounding Flats) that guarantee fault-current safety, survive corrosive subterranean soils, and eliminate premature maintenance overhead?
Manufactured by Omkar Gratings Pvt Ltd (Omkareshwar Engineering), our hot-dip galvanised earthing strips deliver high mechanical rigidity, metallurgical corrosion protection, and strict adherence to international standards including BS EN ISO 1461, IEC 62561-2, and IS 2629. Whether you are laying deep earth grids for 765 kV switchyards, securing utility-scale photovoltaic solar parks against catastrophic lightning surges, or routing protective equipotential conductors in processing plants, our engineered grounding flats deliver verified conductivity, low earth resistance, and zero scrap-theft risk.
Engineered Galvanised Earthing Strips for Power & Industrial Grounding
Grounding conductors must sustain extreme short-circuit fault current surges without thermal deformation or delamination of the zinc protective barrier. Review our recommended production lines engineered for utility power grids, heavy infrastructure, and corrosive soil profiles.
Substation & Switchyard GI Flats
50x6 mm
75x8 mm
75x10 mm
Engineered for electrical transmission substations (33 kV to 765 kV) requiring high thermal capacity under instantaneous earth fault currents (up to 40 kA for 1–3 seconds). Slit from prime low-carbon coil, deburred, and hot-dip galvanized with a minimum 86 microns zinc envelope per BS EN ISO 1461.
Continuous length coil formats (40–50 kg per roll) optimized for rapid trenching, structural tracker bonding, and inverter pad grounding in utility solar fields. Eliminates unwanted intermediate joint welds, lowers total balance-of-system (BOS) capital costs, and completely removes copper-theft vulnerability.
Engineered down-conductors and perimeter grounding rings for chemical processing facilities, refineries, steel plants, and high-rise structures. Provides high mechanical crush resistance against heavy vehicle compaction and soil subsidence while guaranteeing robust equipotential electrical bonding.
An earthing conductor buried below grade experiences a relentless chemical onslaught from soil moisture, dissolved salts, oxygen differentials, and microbial activity. Simple electroplated zinc or painted strip coatings degrade within seasons, triggering accelerated galvanic corrosion of the structural steel core.
Omkar Gratings operates an advanced in-house hot-dip galvanizing bath maintained at a strict 445°C–455°C. When low-silicon, low-carbon steel enters our bath, an authentic metallurgical diffusion takes place, creating four discrete zinc-iron alloy phases (Gamma, Delta, Zeta, and Eta). This guarantees that our Galvanised Earthing Strips possess a surface hardness greater than the underlying base steel, preventing stripping, peeling, or micro-cracking during rough trench backfilling or mechanical uncoiling.
Zinc coating mass verified by digital magnetic gauges and gravimetric stripping tests (IS 6745)
In earthing design, conductor cross-section is fundamentally dictated by maximum expected phase-to-ground fault current ($I_f$), fault duration ($t_f$), and permissible temperature rise ($\Delta T$). According to IEEE Standard 80 and IEC 60364-5-54, steel has a lower electrical conductivity than copper ($\approx 10\%-12\%$ IACS), but its high melting point ($1420^\circ\text{C}$ to $1500^\circ\text{C}$) and mechanical robustness allow engineers to achieve identical or superior fault dissipation by appropriately stepping up the strip's cross-sectional area.
For example, substituting a costly $25\times 3\text{ mm}$ copper flat with a standard $50\times 6\text{ mm}$ Galvanised Earthing Strip yields an equivalent short-circuit fault current carrying capacity while providing four times the cross-sectional mass. This substantial dimensional volume dramatically lowers current density, dampens thermal expansion stress, and offers immense sacrificial reserve against subterranean oxidation.
Low surface touch and step potentials across high-voltage substation grids
High adiabatic withstand rating up to 400°C without core crystal dislocation
Precision de-coiled flats ensure continuous ground contact with zero internal residual curling
Clean Slitting, Deburring & Pre-Punching Zero On-Site Rework for Turnkey Installation
Field installation of grounding grids is expensive and labor-intensive. Rough edges, irregular strip curvature, variable zinc drips, or missing connection holes slow down EPC work crews and compromise mechanical bolt joints. Omkar Gratings eliminates field delays through automated manufacturing workflows.
Our strip processing line uses precision rotary slitting knives to yield burr-free edges, followed by continuous edge radiusing before entering chemical cleaning tanks. For clients requiring prefabricated jumpers or connection risers to equipment pads and lightning masts, we provide CNC multi-hole punching, chamfering, and custom bending prior to hot-dip galvanizing, ensuring an unbroken, impermeable zinc coating over every single hole and cut edge.
Pre-punched bolt holes for standard M10, M12, and M16 earthing lugs
Smooth, unmarred surfaces optimized for exothermic graphite mould sealing
Supplied in compact 40–50 kg roll coils or 6-meter rigid tagged bundles
Future Procurement Trends in Grounding Infrastructure
The global transition to renewable power, hydrogen infrastructure, and automated grid protection is driving fundamental shifts in how global engineering teams procure earthing conductors.
Renewable Energy Expansion
Megawatt-scale solar farms and wind parks demand thousands of linear meters of perimeter grounding. Galvanised earthing strips have become the undisputed standard over copper due to their economic viability and immunity to scrap metal theft on remote installations.
With desert solar installations and coastal offshore converter substations expanding rapidly, EPC tenders frequently reject standard 65-micron coatings in favor of heavy-dip 100–120 micron specifications to combat hypersaline and high-sulfate soil conditions.
Contractors are shifting procurement away from random loose flat bars to factory-cut, pre-punched, and marked earthing assemblies that install directly onto switchgear pads, reducing job-site cutting, welding, and field recoating expenses by over 35%.
Leading EPC procurement teams increasingly source earthing strips, cable trays, and structural gratings from a single integrated producer like Omkar Gratings to ensure uniform galvanizing metallurgy, synchronized logistics, and consolidated MTC compliance.
Modern electrical commissioning demands granular documentation. Every bundle of our GI earthing strip is tagged with mill heat numbers, physical tensile test certificates, chemical ladle analysis, and third-party inspection (TPI) release notes.
Standard Dimensions, Weights & Electrical Sizing Matrix
Cross-sectional reference table for project engineers sizing Galvanised Earthing Strips to withstand expected system short-circuit currents and soil conditions.
Nominal Size (mm)
Cross-Section (mm²)
Approx. Weight (kg/m)
Min. Zinc Coating (μm)
1-Sec Fault Current (kA)
Primary Recommended Application
25 × 3 mm
75.0
0.59
86 μm (610 g/m²)
~6.2 kA
Solar module array bonding, street lighting, small distribution panels
25 × 6 mm
150.0
1.18
86 μm (610 g/m²)
~12.4 kA
Solar inverter stations, lightning protection down-conductors, LT panels
32 × 6 mm
192.0
1.51
86 μm (610 g/m²)
~15.8 kA
Commercial building main earthing ring, motor body grounding
* Note: Fault current ratings calculated in accordance with IEEE Standard 80 adiabatic formula assuming initial steel temperature of 30°C and maximum allowable temperature of 400°C. Custom strip dimensions (up to 100 × 12 mm) and special zinc coating thicknesses available on request.
Global Deployments
Where Our Galvanised Earthing Strips Safeguard Critical Assets
Counterpoise earthing wires and buried earthing flats mitigating lightning back-flashover risk on transmission lines.
Water Treatment & Desalination
High-saline, wet condition earth grids with heavy-spec 100μm zinc layers for long-term immersion safety.
Data Centers & Industrial Parks
Clean earth reference grids ensuring signal integrity, lightning diversion, and personal life safety.
Enterprise Reliability
Quality Assurance & Export Delivery Workflow
Every metric ton of galvanised earthing strip is produced under strict ISO 9001 certified protocols, ensuring total integrity from coil slitting to overseas container discharge.
Prime Steel Slitting
Tested hot-rolled low-carbon steel coils (IS 2062 Grade E250 / S275JR) are rotary-slit with tight edge tolerances and thoroughly mechanically deburred.
Chemical Pre-Treatment
Automated immersion in degreasing, acid pickling, multi-stage water rinsing, and pre-fluxing tanks guarantees an iron-free, clean metallic substrate.
Hot-Dip Galvanizing
Precision immersion in molten virgin zinc bath at 450°C, followed by quenching and dichromate passivation to prevent white rust formation in storage.
Testing & Seaworthy Packing
100% check of coating thickness, adhesion bend test, bundling with steel strapping, and waterproof multi-layer wrapping for heavy ocean freight.
Frequently Asked Technical Questions by Global Buyers
What are the primary advantages of Galvanised Earthing Strips compared to pure copper tape?
While bare copper boasts higher electrical conductivity per unit area, Galvanised Earthing Strips (GI flats) offer superior engineering advantages for ground-grid applications:
1. Cost Efficiency: GI strips provide the required fault-current carrying capacity at 60% to 75% lower total capital expenditure compared to copper conductors.
2. Scrap Theft Elimination: Unlike copper, which suffers epidemic levels of vandalism and theft on remote solar farms and overhead line towers, buried galvanized steel possesses negligible black-market resale value, ensuring permanent ground safety integrity.
3. Mechanical Strength: Steel flats withstand high tensile stresses, heavy mechanical compaction, and subsurface stone shearing that frequently sever softer annealed copper tapes.
4. Sacrificial Corrosion Protection: The zinc coating provides both barrier shielding and cathodic protection, sacrificing itself to shield exposed steel in case of surface gouges or scrapes.
Which international manufacturing and galvanizing standards govern your GI earthing strips?
Omkar Gratings strictly adheres to recognized global standards:
• Base Steel Chemistry: IS 2062 Grade E250 (Fe 410 W), BS EN 10025 Grade S275JR, and ASTM A36 with controlled Carbon (<0.22%) and Silicon (<0.04% to ensure proper Sandelin curve galvanizing).
• Galvanizing Process: BS EN ISO 1461, ASTM A123, and IS 2629 (Hot-Dip Galvanizing Code of Practice).
• Testing & Inspection: IS 2633 (Preece Copper Sulphate Uniformity Test), IS 6745 / ASTM A90 (Weight of Zinc Coating per Square Metre), and IEC 62561-2 (Lightning Protection System Components - Requirements for conductors and earth electrodes).
What minimum zinc coating thickness is recommended for corrosive soil environments?
For benign, high-resistivity soils (>100 Ω·m), an average coating thickness of 70 to 86 microns (500–610 g/m²) is sufficient for a 25-year design life. However, in low-resistivity, aggressive soils (<30 Ω·m) characterized by high moisture, chloride, or sulfate content (common in coastal power plants, tidal zones, and desert agricultural soils), Omkar Gratings supplies heavy-galvanized earthing strips with 100 to 120 microns of zinc coating (850 g/m²). This heavy layer ensures structural survivability exceeding 40 to 50 years.
How does Omkar Gratings prevent embrittlement and guarantee zinc adhesion on earthing strips?
Hydrogen embrittlement is avoided by eliminating excessive acid exposure times during chemical pickling and utilizing proprietary organic pickling inhibitors. The steel is thoroughly rinsed and dried prior to immersion. Coating adhesion is verified by rigorous mechanical testing: pivoting hammer tests (IS 2629) and 90-degree cold bend mandrel tests ensure that the intermetallic alloy layers do not flake, peel, or blister under high stress.
Can GI earthing strips be welded on-site without destroying corrosion protection?
Yes. In earth-mat installations, GI strips are joined using either overlapping shielded metal arc welding (SMAW) or exothermic graphite mould reactions. An overlap of at least twice the width of the strip is engineered for full electrical and mechanical transfer. After welding, the weld joint must be chipped clean of slag and immediately recoated with a zinc-rich epoxy paint or cold-galvanizing aerosol containing at least 90% dry zinc dust per ISO 12944 or ASTM A780, restoring complete corrosion resistance.
How are earthing strips bundled and preserved against white rust during sea freight?
Ocean voyages expose steel cargo to high humidity and salt vapor, which can cause wet storage stain (zinc hydroxycarbonate / white rust) if water enters tightly nested bundles. To safeguard export shipments, all earthing strips undergo post-galvanizing passivation via a sodium dichromate bath. Finished coils or straight bars are wrapped with volatile corrosion inhibitor (VCI) paper, enclosed in heavy-duty HDPE waterproof woven fabric, strapped tightly with tensioned steel bands, and mounted onto treated wooden skids with desiccants inside the shipping container.
Need Certified Galvanised Earthing Strips for Your Next Project?
Send your bill of quantities (BOQ), sizing requirements, or tender specifications. Our technical engineering and sales team will provide competitive factory-direct pricing, mill certificates, and delivery timelines.