1 / 5
Our cable trays strictly comply with international quality and safety benchmarks, including CE and ISO certifications, meeting engineering requirements for large commercial and industrial projects worldwide.
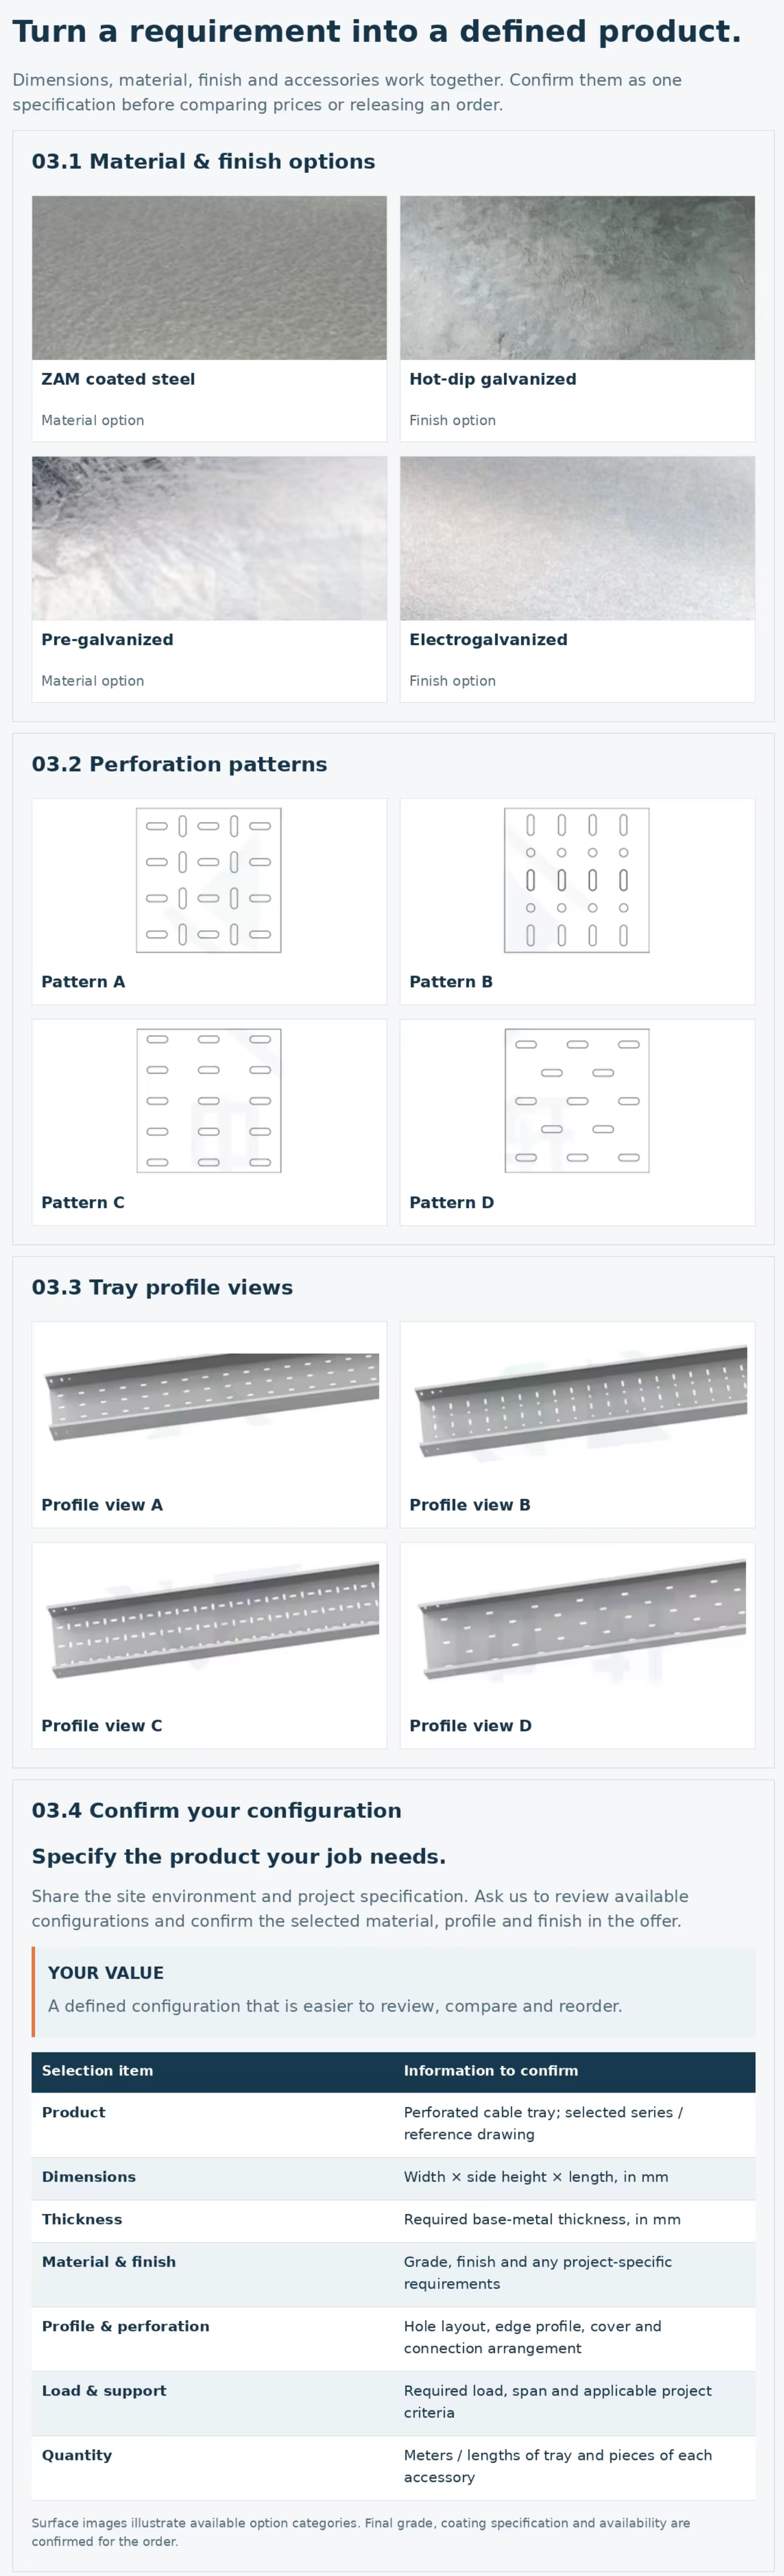
We provide a thick, uniform zinc coating exceeding 65μm, ensuring robust corrosion resistance and oxidation protection even in challenging marine, chemical, or humid outdoor settings.
Thanks to the heavy-duty hot-dip galvanizing and high-grade steel construction, our cable trays can achieve a service life of more than 25 years in harsh conditions such as mining, coastal areas, and oil & gas installations.
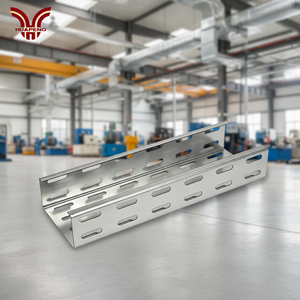
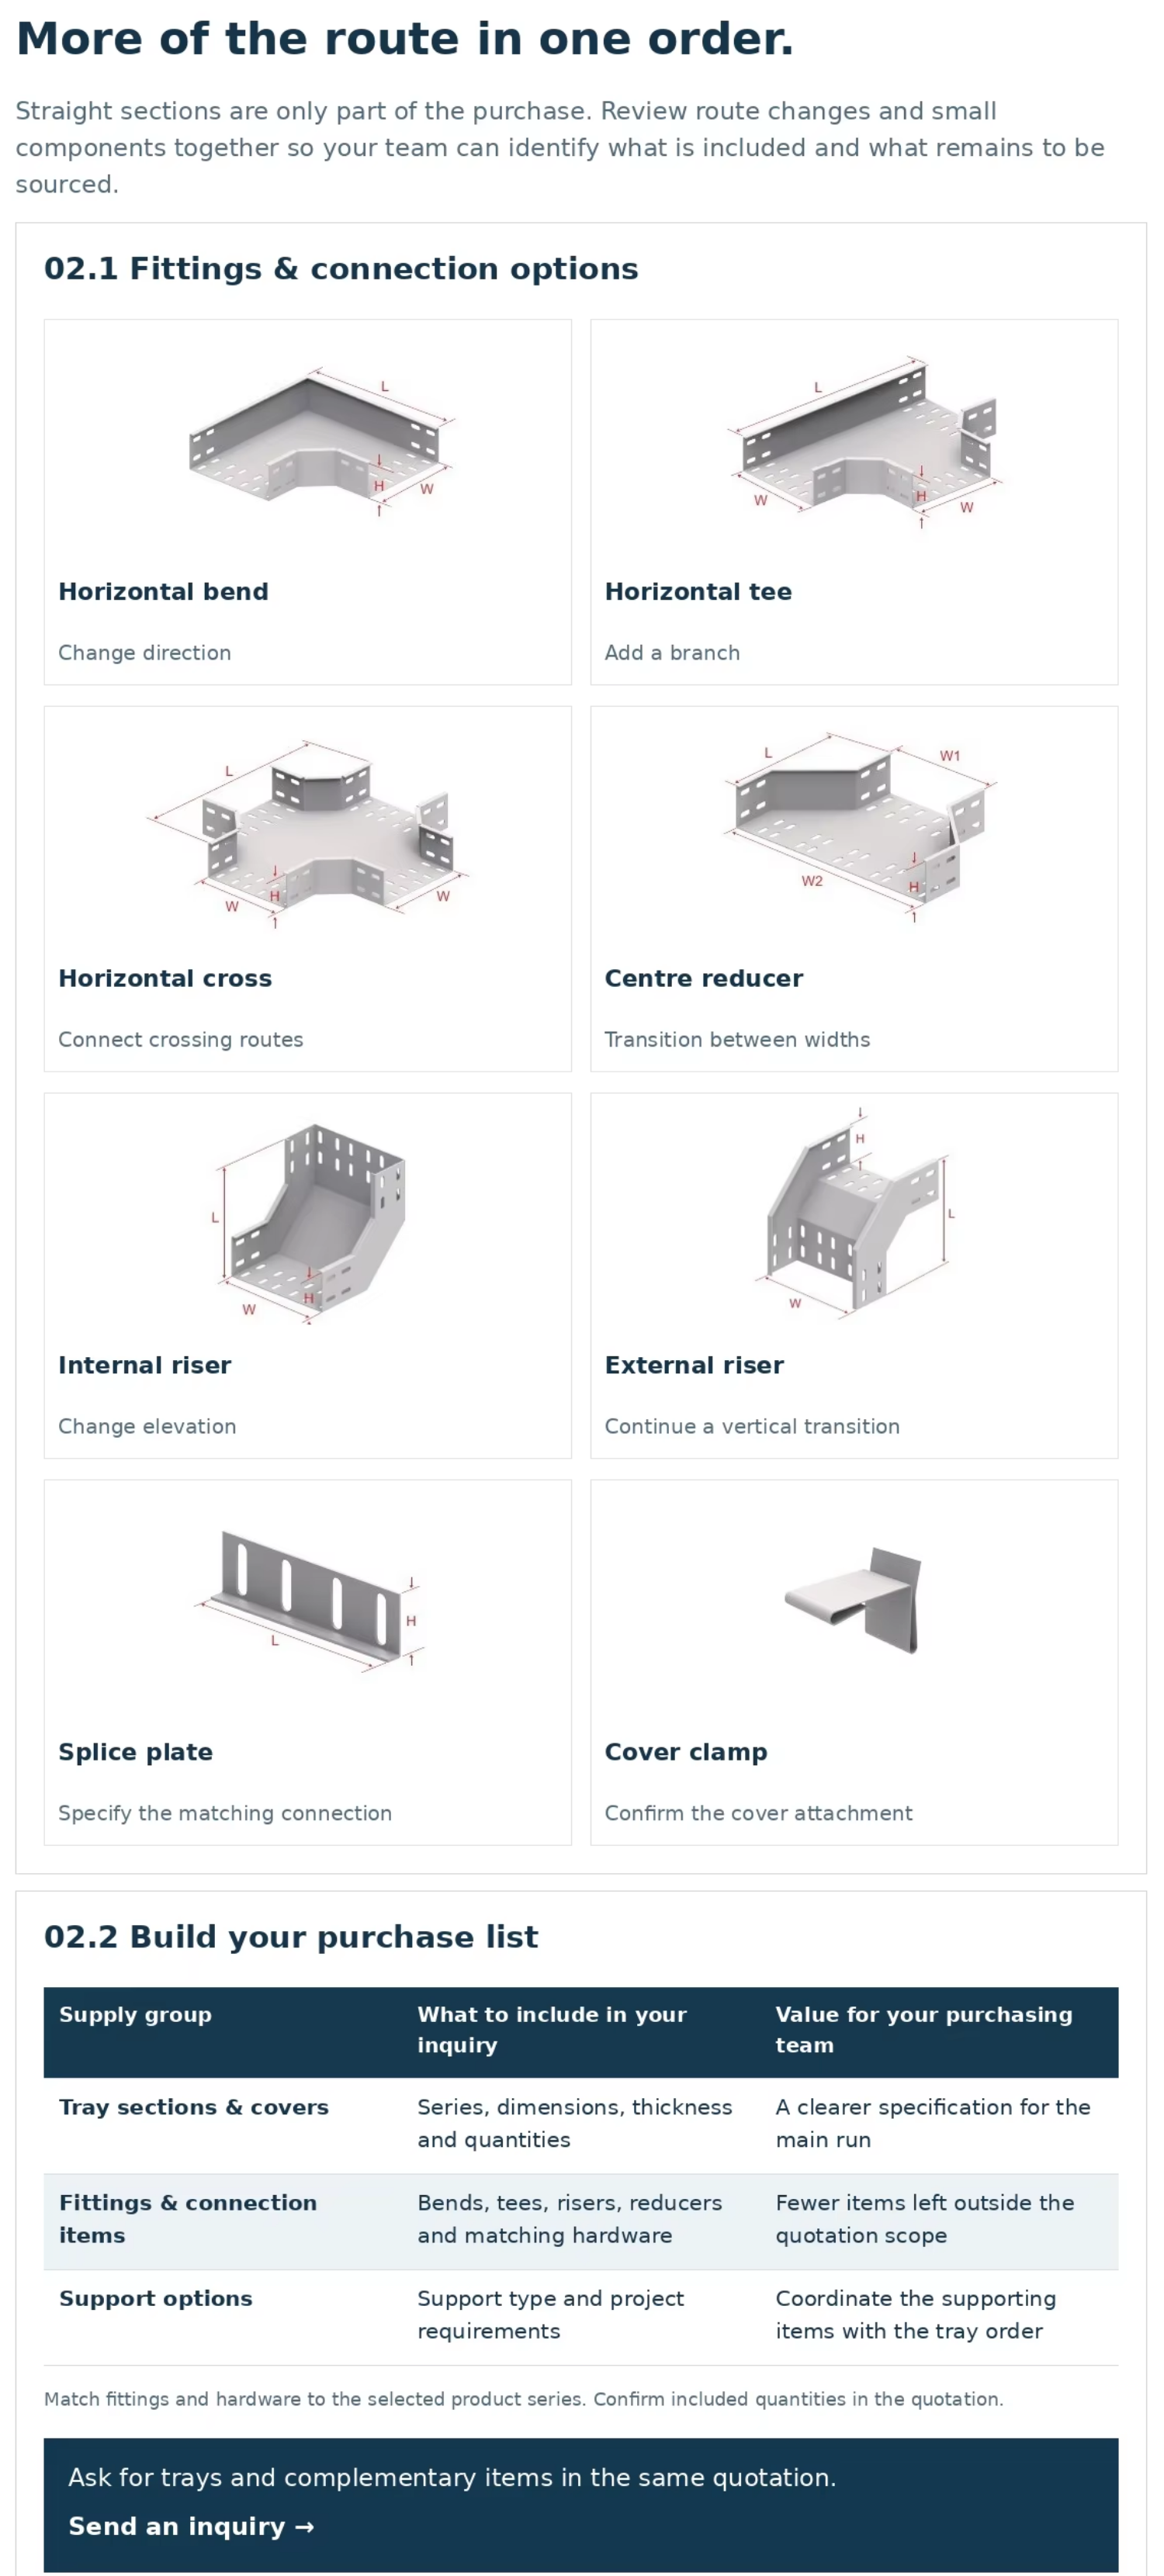
Yes, as a specialized manufacturer, we offer comprehensive customization for dimensions, material thickness, hole patterns, and accompanying accessories tailored to your engineering project needs.
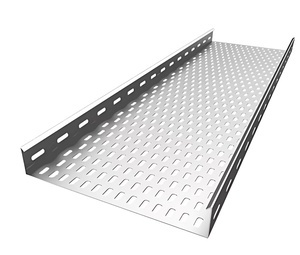
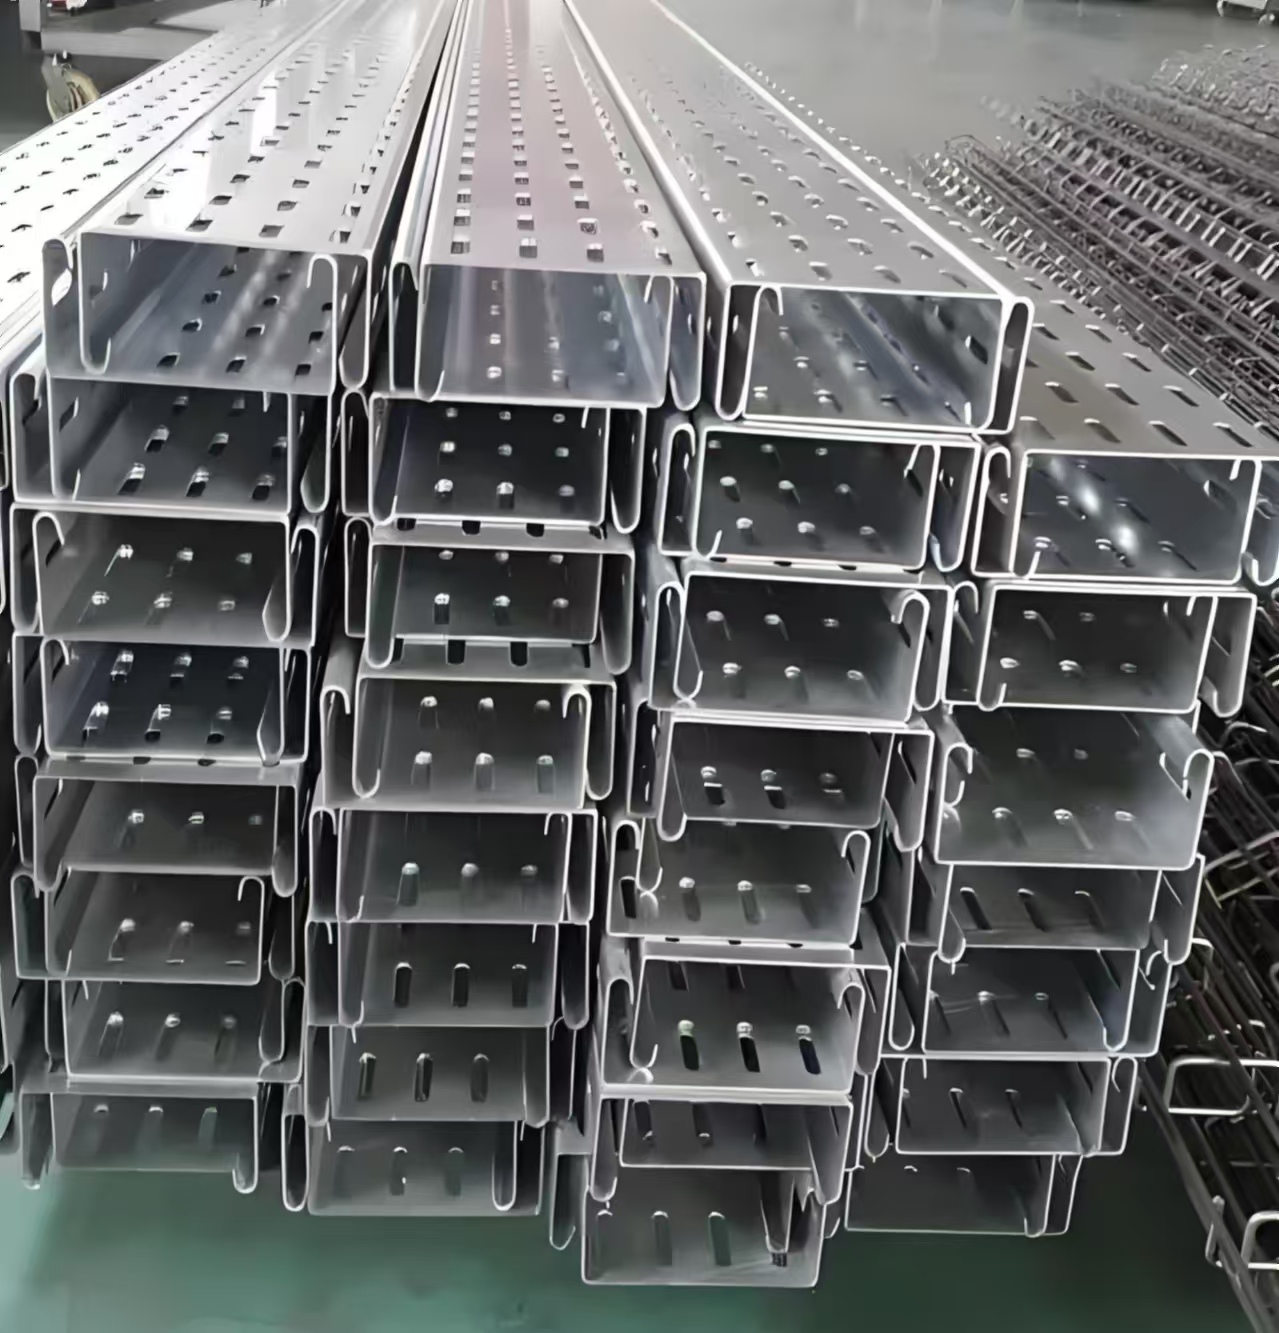
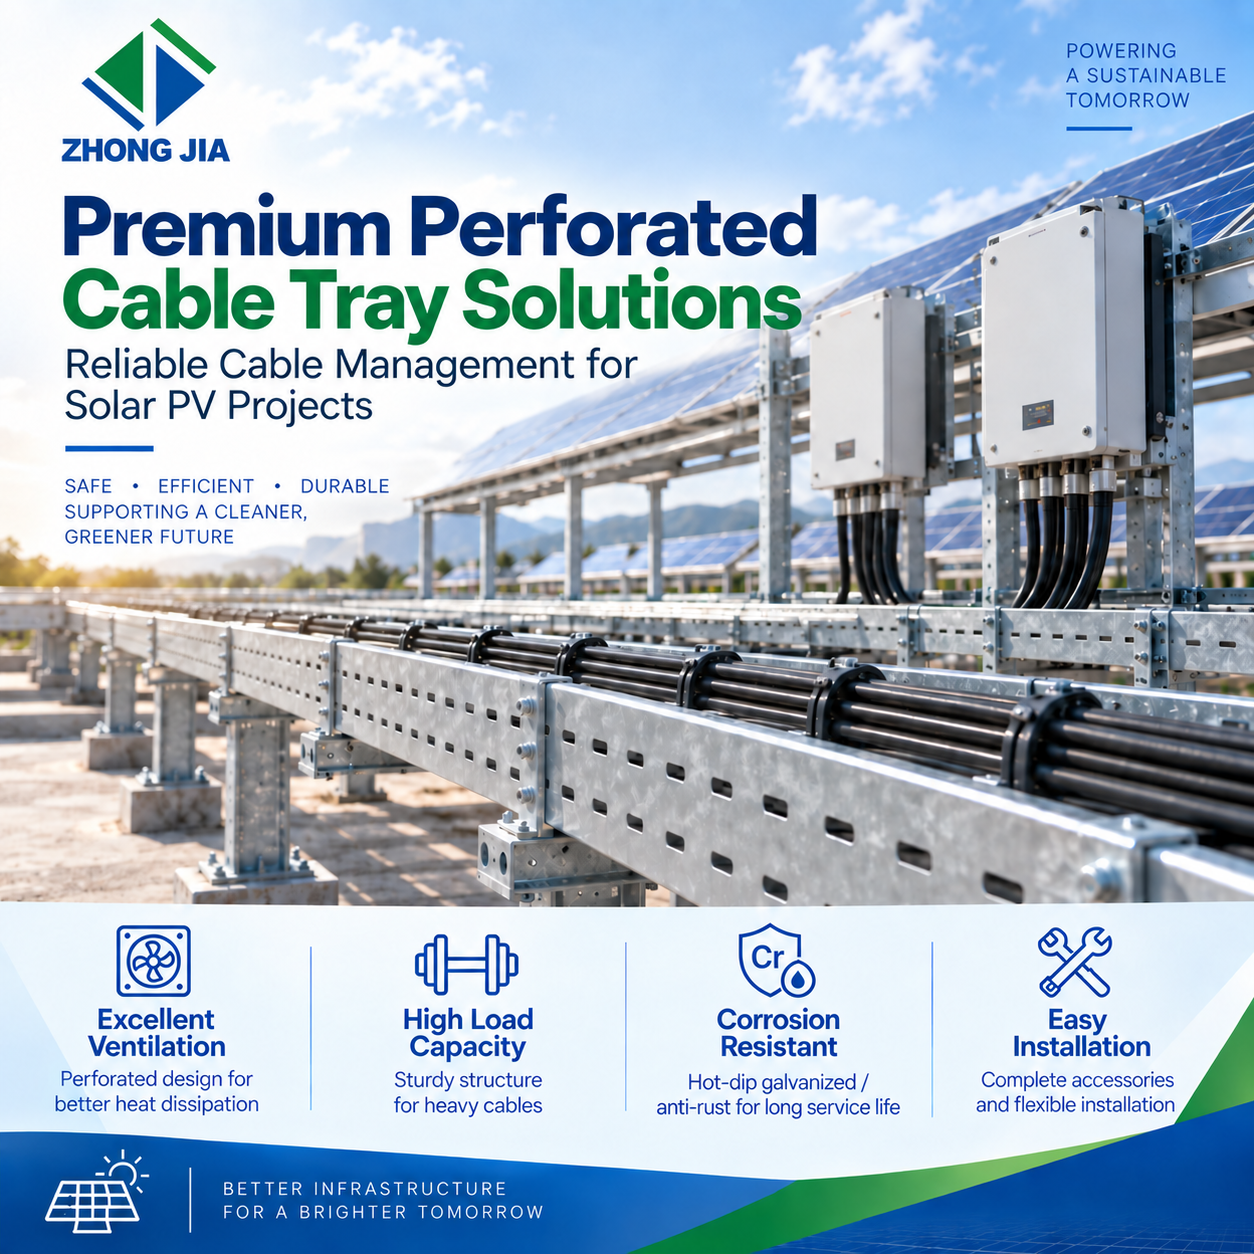
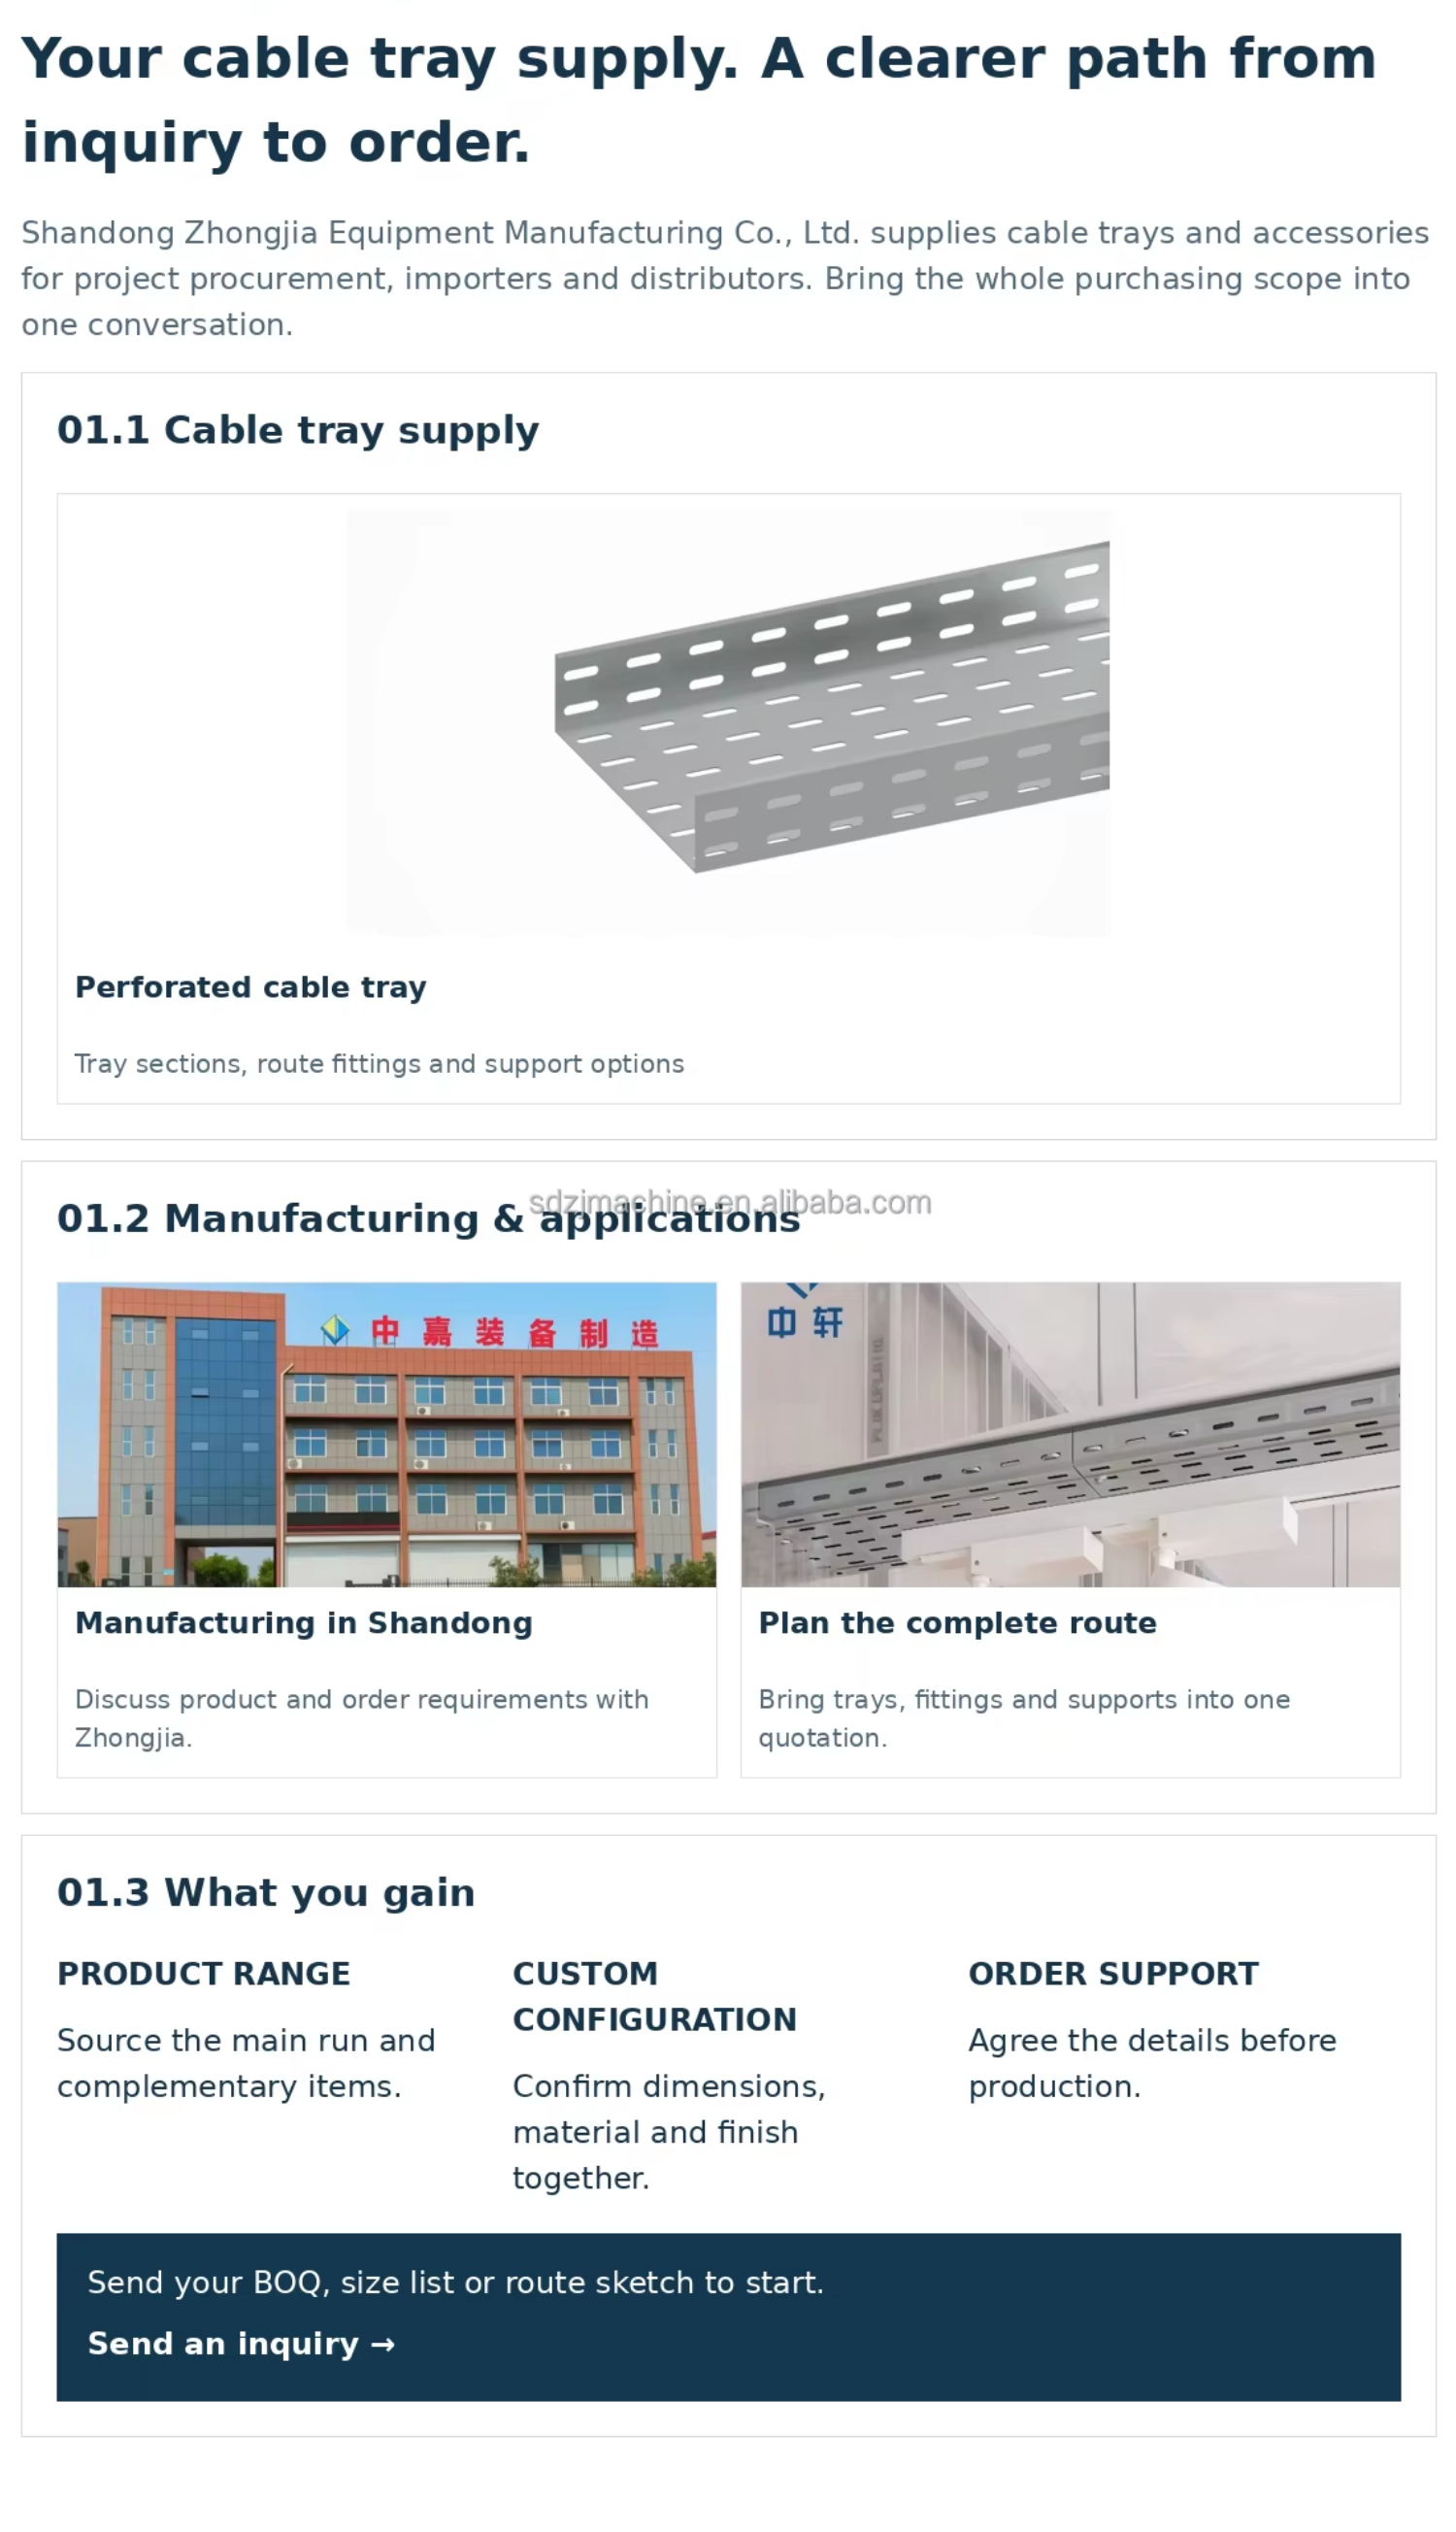
The precision perforations maximize continuous airflow around the cables, significantly enhancing heat dissipation for power cables while maintaining high structural strength and reducing overall tray weight.
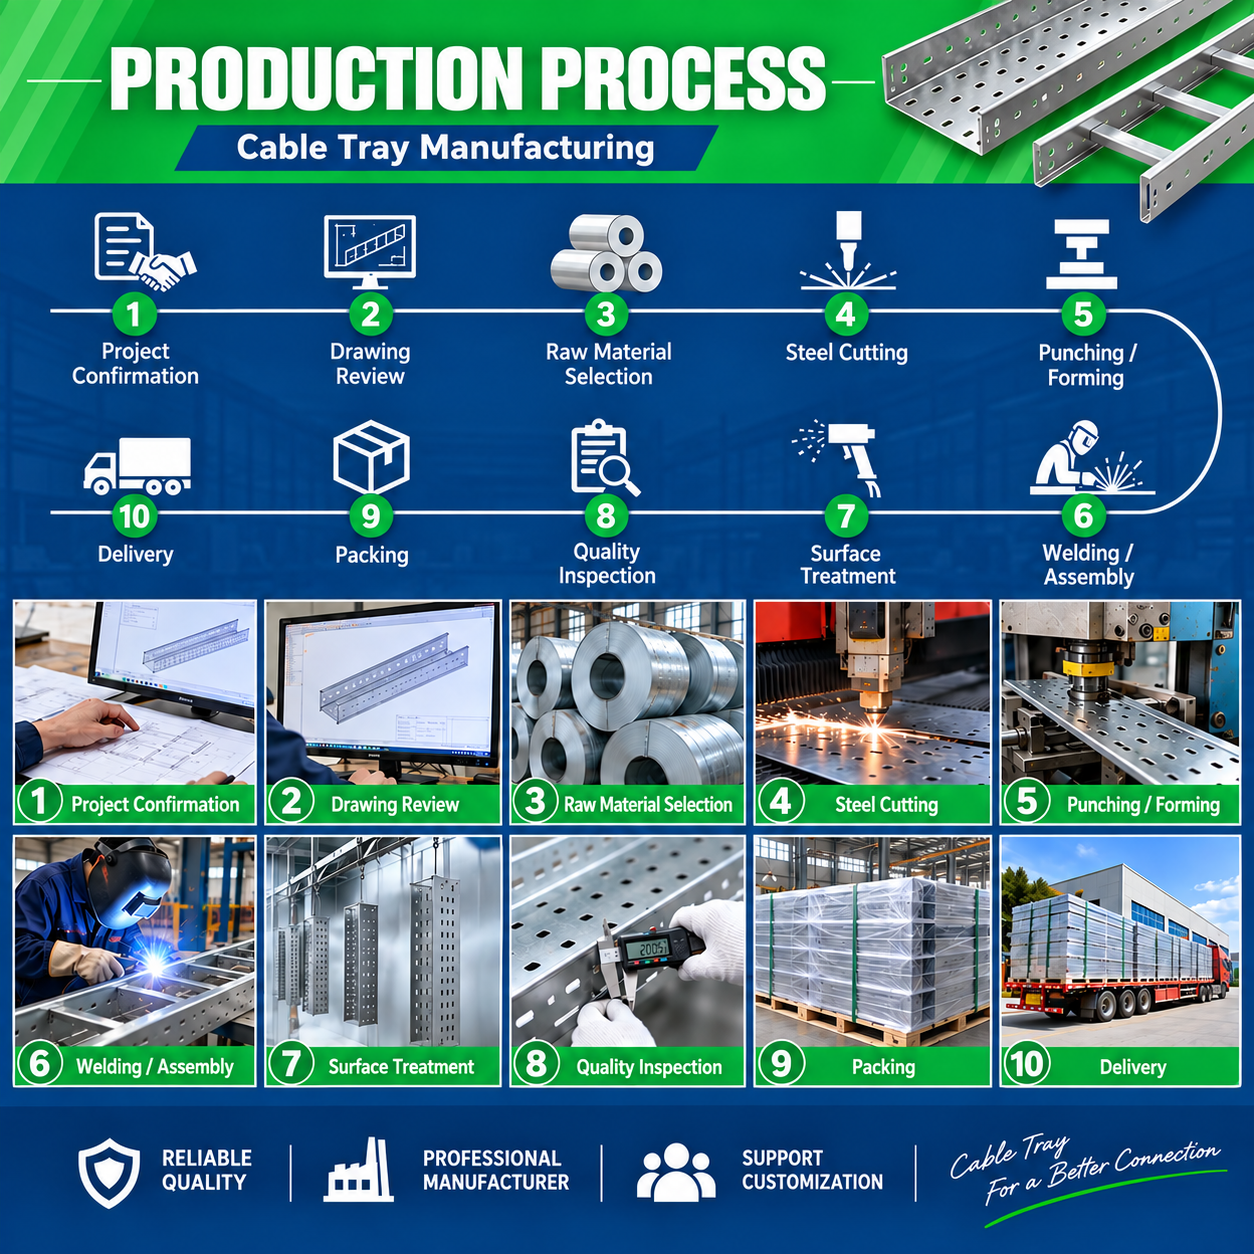
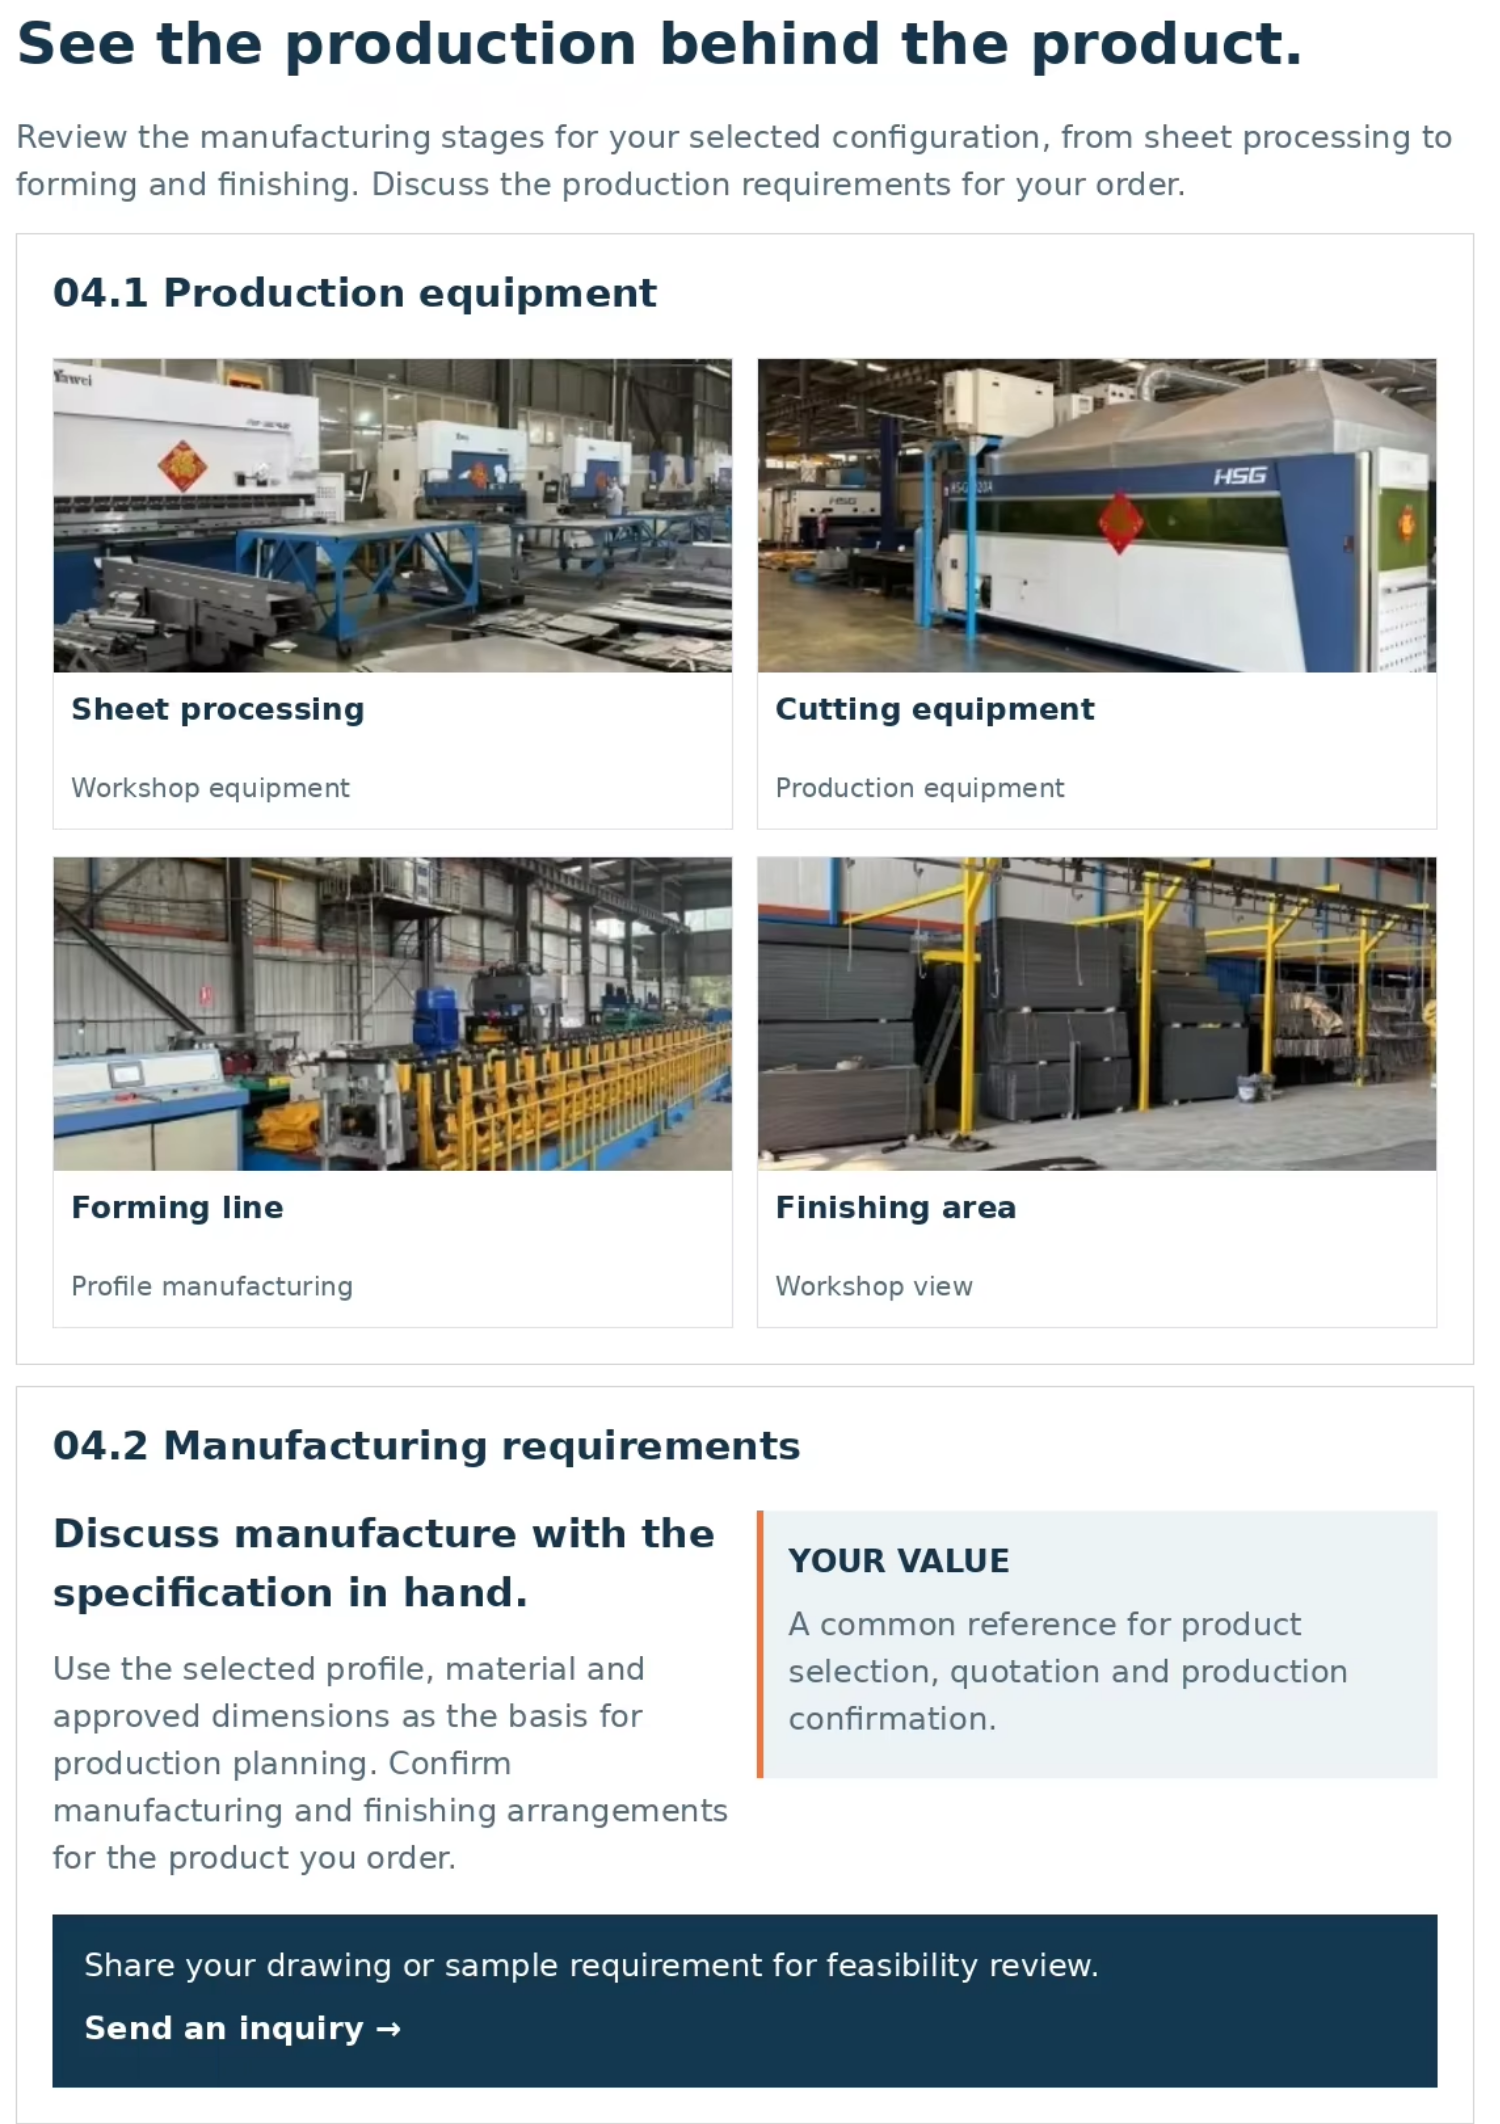
Our manufacturing process includes precise deburring to ensure completely smooth, burr-free edges, preventing cable sheath damage and ensuring safe handling for installation teams.