
Built for EPC infrastructure, offshore platforms, municipal trench networks, chemical process galleries, and logistics mezzanine structures with certified deflection load ratings.
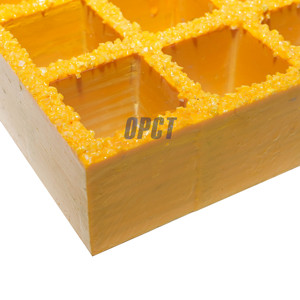
Molded structural fiberglass composite featuring bi-directional load bearing, superior chemical inertia, fire-retardant vinyl ester resins, and embedded silica grit anti-slip treads.
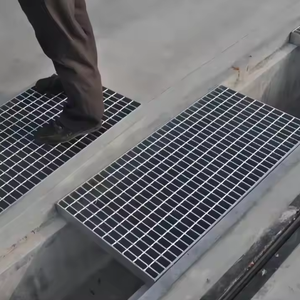
Electroforged open grid platform mesh hot-dip galvanized to ASTM A123 standards. Designed for elevated mezzanine paths, civic parks, outdoor stages, and maintenance walk rings.
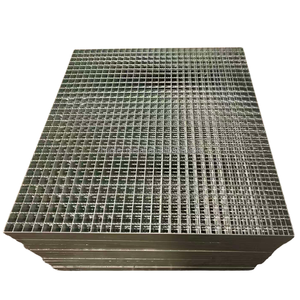
High-micron zinc protective layer engineered for extreme weathering on architectural structures, rooftop HVAC platforms, mechanical walkways, and commercial plant infrastructure.
Certified structural grade carbon steel for heavy drainage trenches, cooling tower surrounds, electrical power station galleries, and industrial runoff management flumes.
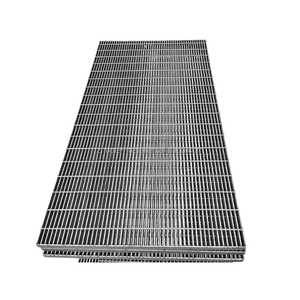
Global standard pitch configuration optimizing steel density, light ingress, and lateral rigidity for multi-tier warehouse walkways, crane corridors, and access runways.
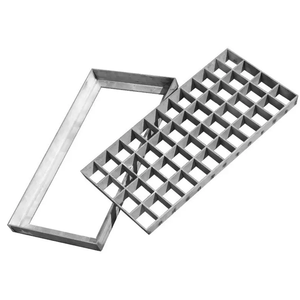
Pressure-welded austenitic stainless steel acid-pickled and electro-polished. Unrivaled pitting resistance for maritime jetties, chemical refining decks, and cleanroom plants.
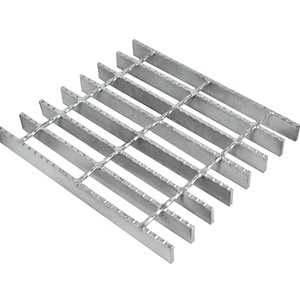
Heavy profile bearing bars engineered for combined wheel loading and pedestrian passage across loading terminals, municipal depots, airport staging ramps, and industrial yards.
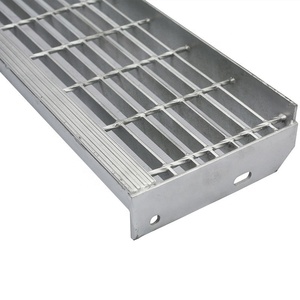
Factory welded with pre-punched bolting end-plates and serrated cast checker-plate visual nosing. Designed for rapid job-site installation on industrial emergency egress stairs.
Combining heavy-tonnage automated electroforge technology, multi-axis computerized plasma profiling, and end-to-end metallurgical quality control.
Our heavy-duty automated forge welding applies hydraulic compressive forces exceeding 100 tonnes while driving a 2,200 Ampere electrical current into the intersection points. Twisted square cross bars penetrate deep into solid bearing flats without filler rod, delivering continuous molecular fusion free of internal gas pockets, thermal cracking, or notch-stress concentrations.
Industrial layouts require complex geometry to bypass vertical pipelines, H-columns, and valve manifolds. Every circular, square, or skewed cut-out is mechanically plasma-cut and edged with full perimeter flat bar banding welds. This locks the load-bearing bars together, preventing mechanical deflection and complying with stringent OSHA toe-plate safety codes.
We operate proprietary galvanizing kettles adhering rigorously to ASTM A123, ISO 1461, and BS EN ISO 1461 standards, creating zinc alloy diffusion layers up to 85–100 microns thick. For specialized austenitic stainless applications (AISI 304, 316, 316L, 309), acid-pickling and electrolytic polishing treatments eradicate weld discoloration and restore an impervious chromium oxide passive layer.
Our programmable rolling lines produce panel widths ranging from 250 mm to 1200 mm, with span lengths tailored precisely to client structural steel drawings. Controlled heat dissipation ensures near-zero camber and diagonal variance (±2 mm), eliminating the need for costly on-site torch cutting, thermal distortion repair, or structural modifications during plant assembly.
All structural raw materials (Q235, S275JR, ASTM A36, AISI 304, AISI 316) enter production accompanied by heat lot inspection certificates. Every dispatch parcel is tagged with unique barcode identifiers linkable directly to raw material mill sheets, tensile elongation test results, ultrasonic defect screening reports, and zinc thickness gauges.
Export parcels feature high-tensile steel strapping, bottom timber runners, corner edge guards, and waterproof wrapping to withstand ocean container routes. Every bundle is pre-indexed and marked according to erection drawings, allowing field teams to hoist panels straight from dock containers directly onto overhead steel framing.
Cross-reference your environmental corrosion exposure, span distances, and concentrated pedestrian vs vehicular loads.
| Grating Classification | Alloy & Material Grade | Structural Joining Process | Standard Surface Finish | Primary Industrial Use-Case |
|---|---|---|---|---|
| Standard Electroforged Bar Grating | Q235, S275JR, ASTM A36 Low Carbon Steel | PLC Electroforged Resistance Fused (No filler metal) | Hot-Dip Galvanized (≥610 g/m²), Self-Colour, Bituminous | Power generating halls, boiler towers, catwalk walkways, pipe bridges |
| Corrosion-Proof Stainless Grating | AISI 304, AISI 316, 316L, 309 Stainless Steel | Hydraulic Pressure Welded / TIG Welded Assembly | Nitric-HF Acid Pickling, Electro-Polished, Bead Blasted | Offshore drilling decks, pharmaceutical cleanrooms, chemical tanks |
| Heavy-Duty Vehicle Traffic Mesh | High-Yield Structural Carbon Steels (5mm–10mm bars) | Double-sided CO2 Gas Shielded Submerged Arc Welds | Heavy Micro-Galvanized, Black Uncoated Primer | Logistics ports, municipal road gutters, airfield taxiways, forklift ramps |
| Structural Molded & Pultruded FRP | Isophthalic / Vinyl Ester Resin with Continuous E-Glass | One-piece Heated Compression Mold Matrix | Concave Anti-Slip Meniscus, Coarse Quartz Grit Embedded | Acid pickling lines, marine piers, wastewater clarifiers, battery rooms |
| Expanded Metal Diamond Catwalk | Carbon Steel, Austenitic SS, Marine Aluminum | Simultaneous Slit & Cold Die Expansion Process | Galvanized, Anodized, Architectural Powder Coated | High-level suspended service catwalks, ceiling maintenance grids, sun louvers |
| Custom Cut-Out Fabricated Panels | Mild Steel, Structural Stainless, Aluminum 6061-T6 | Hand Fabricated, CNC Laser Profiled, Fully Banded Edges | Zinc immersion, Epoxy barrier painted, Passivated | Turbine access balconies, valve station decks, pipe penetrations |
For standard pedestrian paths, a uniform working load (UDL) of 5.0 kN/m² or a concentrated center load (point load) of 1.5 kN over a 200x200mm area is typically specified. Our technical engineering division validates deflection limits under L/200 or 4 mm (whichever is lesser) to prevent foot bounce and ensure worker ergonomics.
Where oil mists, condensation, or grease are present, flat bearing bars can be modified with deep-milled serrations. This creates aggressive gripping points exceeding DIN 51130 R11–R13 slip resistance requirements, drastically mitigating slip-and-fall hazards on petrochemical stair towers and marine gangways.
When installing stainless steel or carbon steel gratings directly on aluminum or painted structural steel stringers, our OEM package supplies neoprene insulating pads and stainless 316 M-clips with nylon isolators to prevent galvanic corrosion cells and prolong platform service lifespans.
How international procurement managers, EPC engineering directors, and project estimators are optimizing their supply chains.
Procurement teams are moving away from manual 2D CAD cut-sheet approvals. Modern contracts demand direct BIM (Building Information Modeling) file imports (IFC, Tekla, Revit). Our automated systems translate client 3D structural models into CNC cutting and banding coordinates, eliminating human reading errors, reducing manufacturing lead times by 35%, and ensuring zero-clash installation around complex process piping.
Procurement audits look beyond the FOB initial price per square meter. In harsh environments, premature failures of low-grade coatings drive massive maintenance shut-downs. Buyers increasingly opt for heavy-coat galvanizing (>85 microns) or hybrid dual coatings (thermal zinc spray + epoxy topcoats) that offer 30-year zero-maintenance life, yielding substantial lifecycle savings over cheaper, thin-dipped alternatives.
Global supply chain volatility has pushed multinational contractors to favor OEM partners with large buffer stocks of primary raw coils and automated high-output PLC machinery. Our integrated fabrication capacity guarantees stable project schedules, allowing fast shipping to key infrastructure hubs across Europe, North America, the Middle East, and Southeast Asia.
International environmental and green-building codes (LEED, BREEAM) now require verified scrap steel ratios and low-emission production records. We utilize EAF (Electric Arc Furnace) steel billets that incorporate up to 80% recycled ferrous scrap alongside energy-efficient induction furnaces, providing verified Environmental Product Declarations (EPDs) for modern ESG compliance.
Next-generation metallurgical coatings, composite lightweighting, and automated safety monitoring systems.
Traditional pure zinc galvanizing is rapidly evolving toward continuous Zn-Al-Mg bath formulations. ZAM coatings provide three to five times higher corrosion resistance than conventional hot-dip zinc in aggressive salt-spray and acidic air. Moreover, the aluminum and magnesium in the coating dissolve slightly to form a self-healing film over freshly cut edges, eliminating site-touch-up vulnerabilities.
To reduce topside weights on offshore oil rigs and green-hydrogen coastal platforms, hybrid pultruded gratings combine carbon fiber cores with vinyl ester outer shells. These lightweight panels match the stiffness of structural carbon steel at one-fourth the weight, significantly reducing load requirements for supporting steel frames while remaining immune to seawater pitting.
Manual stick welding of border bands is giving way to multi-axis robotic welding cells. Automated tracking delivers uniform fillet sizes, complete root penetration, and a splatter-free surface finish. This clean fabrication base ensures uninterrupted galvanizing coverage, prevents sharp zinc run-off spikes, and enhances safety for workers handling panels on site.
Technical guidance covering manufacturing tolerances, load engineering, specification writing, and export compliance.
Electroforged gratings are manufactured using automated PLC systems that combine massive hydraulic pressure (exceeding 100 metric tonnes) with a high-current electrical pulse (~2,200 Amperes). This fuses the square twisted cross bar directly into the pre-slotted bearing bar at the molecular level, creating a seamless joint without any filler metal. Key benefits include:
Manually welded gratings are assembled using CO2 gas metal arc welding (GMAW). While ideal for small production runs, irregular shapes, or heavy-duty flat bars exceeding 7mm in thickness, manual welding exhibits higher thermal stresses and minor dimensional variances compared to automated electroforging.
Alloy selection depends on operating temperatures, chloride exposure, and ambient chemical concentrations:
While galvanized steel provides high modulus of elasticity and cost-effective long spans, Fiberglass Reinforced Polymer (FRP) is preferred in specialized operating conditions:
Yes. OEM/ODM custom fabrication is our core specialty. We manufacture custom panels from client structural layout drawings (DWG, DXF, or BIM formats):
To provide a definitive quotation, our engineering team requires the following parameters:
Connect with our technical grating application engineers. Send your CAD drawings, bill of materials, and specifications for a rapid review, load calculations, and competitive OEM/ODM manufacturing terms.